


Cnc Aluminum Keyboard Parts Electronic Keyboard Enclosure
Specifications: customized according to the requirements of drawings and samples
Introduction: Professional hardware accessories processing factory
Description
Technical Parameters
OEM aluminium cnc milling service machining cnc aluminum wallet parts

Product Description
Shenzhen pride Industrial Co., Ltd. is a solution provider specializing in high-precision parts and hand forming.
The company is proficient in all kinds of aluminum alloy, stainless steel, titanium alloy, plastic and other materials of special-shaped / complex / high-precision hand model processing, mainly used in rail transit (automotive hardware), digital electronics, medical equipment, artificial intelligence, smart home and other fields.
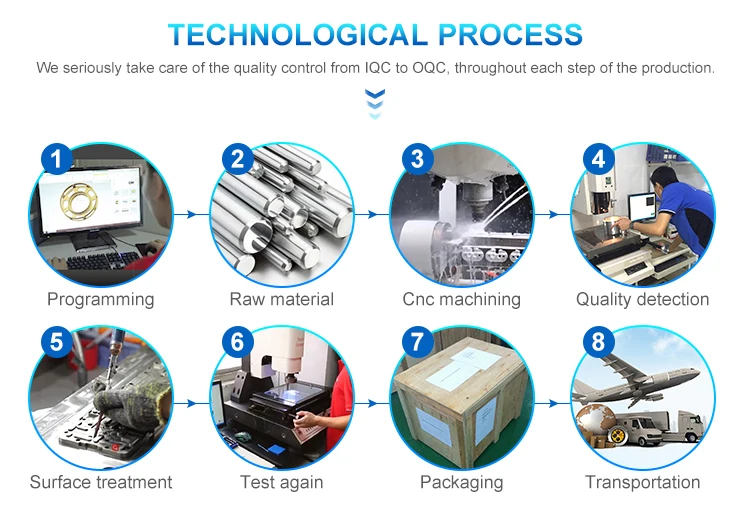
Production process covers: CNC machining, CNC metal processing, CNC lathe processing, metal stamping, plastic injection , mold processing.
Available Material (metals) | Available Material (plastic) | ||
Alloy (aluminum, zinc, magnesium, titanium) | ABS, PC,ABS, PMMA (acrylic), Delrin,POM | ||
Brass, bronze, beryllium, copper | PA (nylon), PP, PE, T | ||
Carbon steel, stainless steel, SPCC | Fiberglass reinforced plastics, Teflon | ||
Processes | Surface treatment (finish) | ||
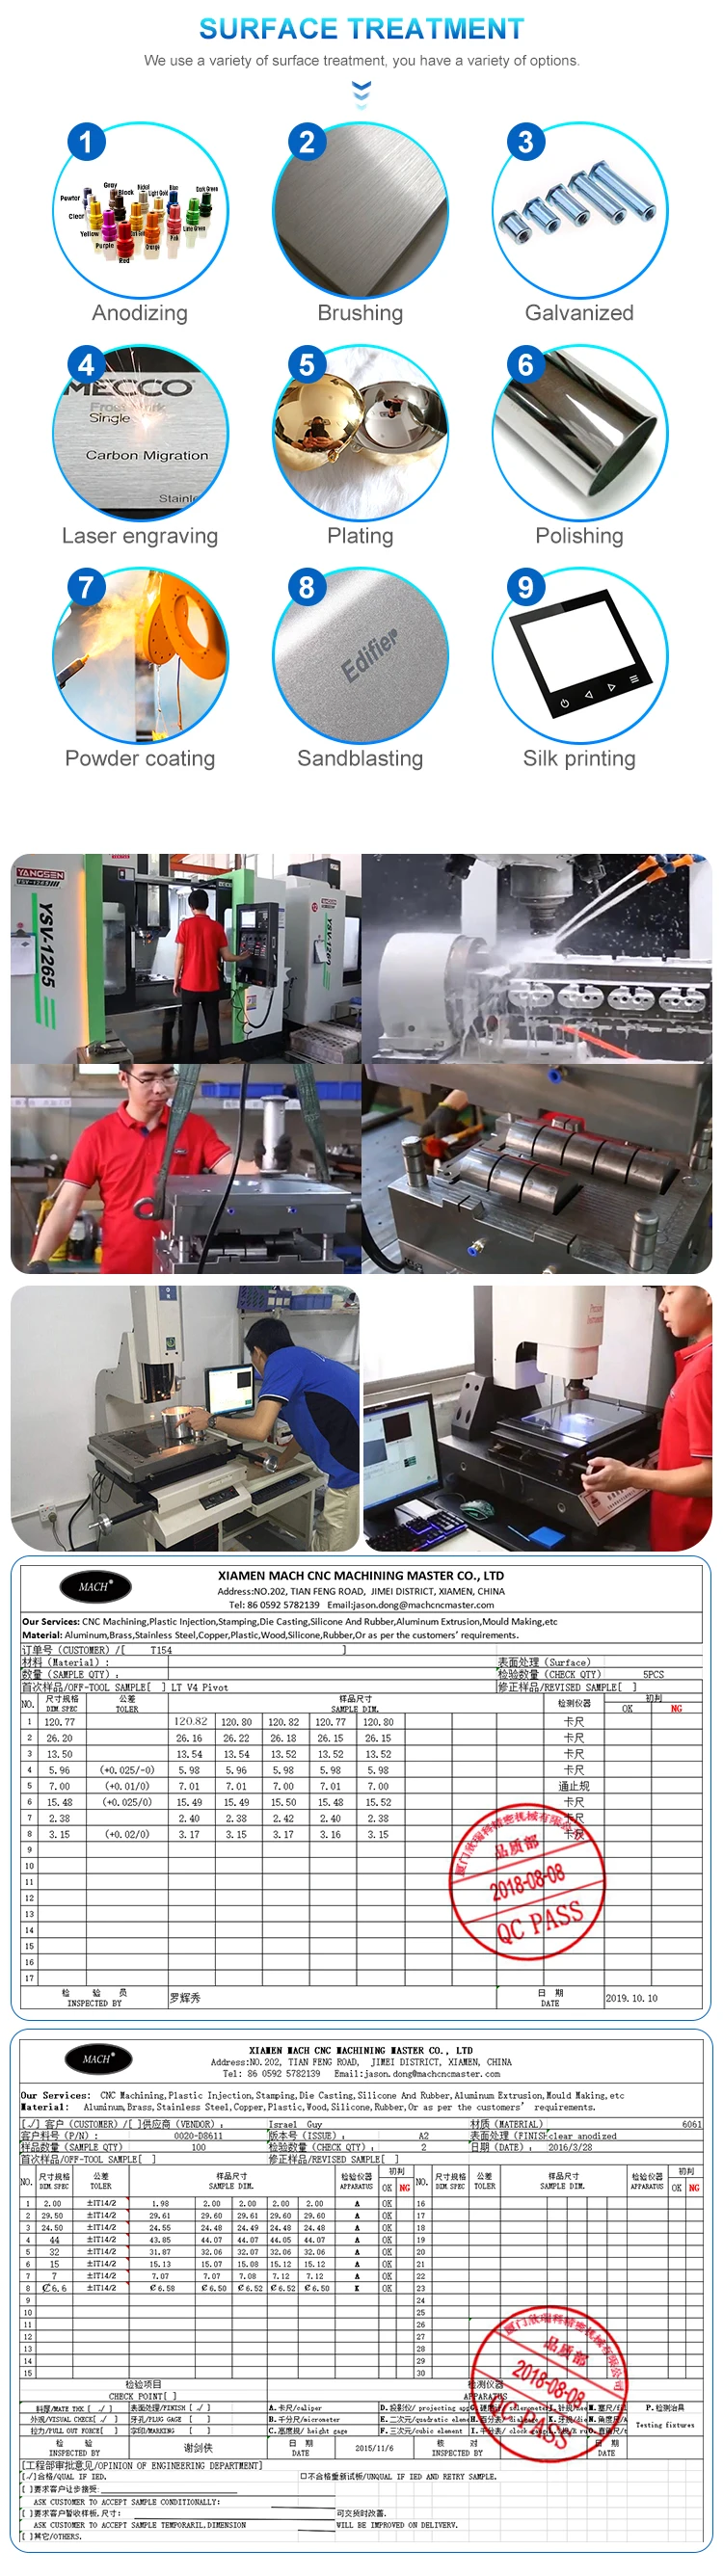
CNC machining(Milling/Turning), Grinding | High polish, brush, sand blast, anodization | ||
Sheet metal stamping, bending, welding, assembly | plating (nickel, chrome),powder coat, | ||
Punching, Deep drawing, Spinning | Lacquer painting, , silk screen, pad printing | ||
Equipment | Application | ||
CNC machining centers (FANUC, MAKINO) | CMM (3D coordinate measuring machine), 2.5D projector | ||
CNC turning centers/ Lathes / Grinders | Thread gauge, hardness, caliber. A closed-loop QC system | ||
Punching, Spinning and Hydraulic tensile machines | Third party inspection available if required | ||
Lead time & Packing | Application | ||
7~15 days for sample, 15~25 days for production | Automotive industry / Aerospace/ Telecom equipment | ||
3~5 days via express: DHL, FedEx, UPS, TNT, etc. | Medical / Marine / Construction / Lighting system | ||
Standard export carton with pallet. | Industrial Equipment & Components, etc. |


 | 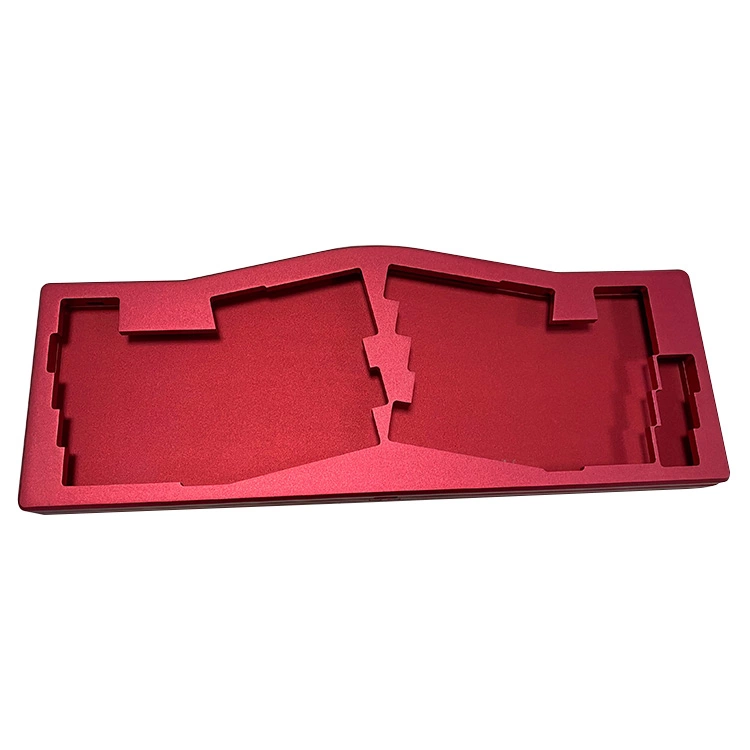 |
| Black anodized | Red anodized |
 |  |
| Gray anodized | silver anodized |
 |  | 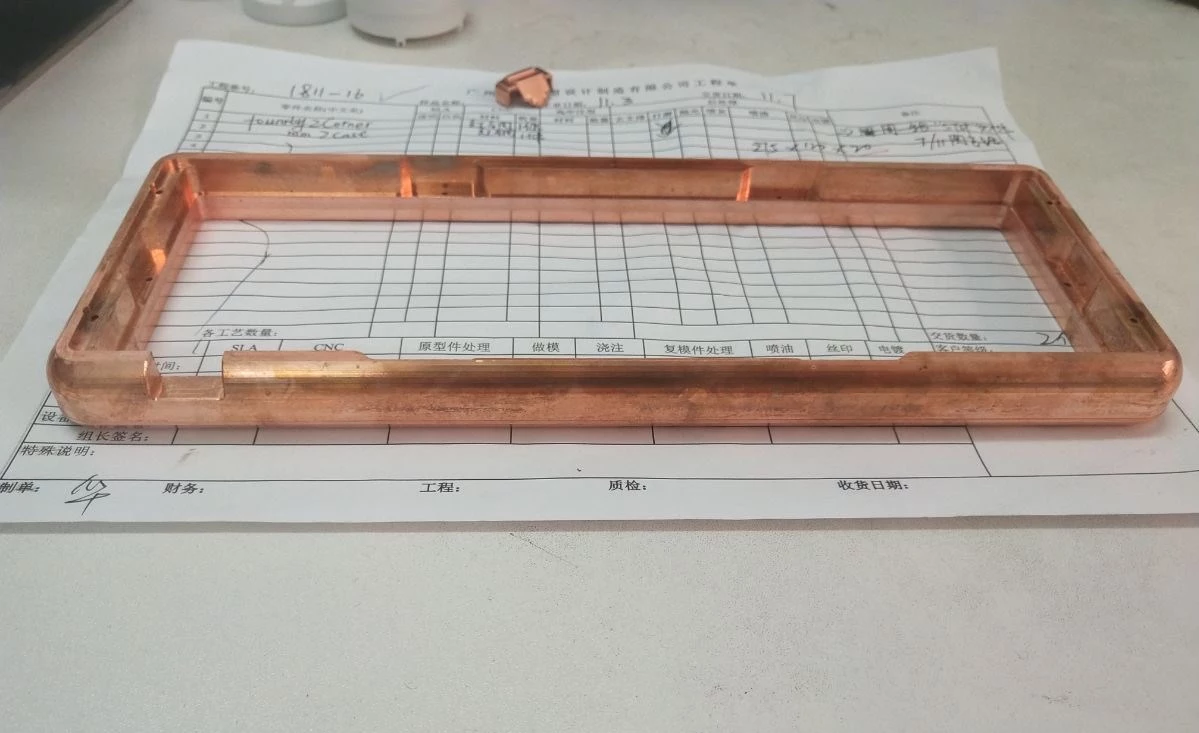 |
| pc | Acrylic | Copper |
Mold Design:
For sand casting, the mold is made of wood or other metal materials. In this process, we asked our engineers to make the mold size slightly larger than the finished product, and the difference is called the shrinkage allowance. The purpose of this is to melt the metal into the mold to ensure that the molten metal solidifies and shrinks, thereby preventing voids in the casting process.
Core Making: The core is formed by casting resin sand into a mold to form a casting of the inner surface. Therefore, the gap between the core and the mold eventually becomes a casting.
Casting Producing: A mold is required during the smelting process. Molding typically involves the support frame of the mold, which is pulled out to separate during the casting process, where the previously placed core melts in the mold and then closes the die opening.
Cleaning & Machining: The purpose of cleaning is to remove sand, sand and excess metal in the casting. Welding, sand removal can improve the appearance of the casting surface by burning the sand and the scale is removed to improve the appearance of the surface of the casting. Excess metal and other risers are removed. A step further by welding and grinding. Some castings are subject to special post-processing requirements such as heat treatment, shaping, anti-rust treatment, roughing, etc. Finally, Checking the defects and comprehensive quality finishing, before processing, and then re-processing, according to the requirements of different customers, we can do heat treatment, surface treatment, additional inspection and so on.
![Q@~2R~6G01YDJ$O]ARS5L$N](https://www.pride-cnc.com/Content/uploads/2020572095/20200720120052e584557864a84b66ae9d58aa686cb61e.png)
Our Company


Packaging
1,carton packing
2,wooden box
3,plastic bag
4,As your requirements

Shenzhen pride Industrial Co., Ltd.
Tel:+8618666663894
Fax:+86-917-3387002
Mob:+86-755-23699351
E-mail: crush@pride-cnc.com
Add: Block D, Dianlian Science Park, Matian St., Guangming District, Shenzhen 518106, China
Latest News
Control the size of the bright band of the part fracture to control the chip generation
Trimming clearance
Our company's original aluminum plate production experience is not rich. The cutting edge clearance is roughly the same as the steel plate, which is 8% of the material thickness. However, according to the soft characteristics of the aluminum plate, the 8% clearance makes the bright band of the fracture account for about 2/3. This produces some burrs, which are easily rubbed off during the flanging process. Form chips. We later consulted foreign standard parts manuals to optimize the trimming gap. The trimming gap is 10%-12% of the thickness of the sheet. According to this feature, the knife edge is trained. Ensure that all gaps are consistent. In order to avoid rubbing the fracture again after trimming. We make the cutting edge perpendicularity to -2°, and the cutting edge roughness reaches Ra0-20.4um.
Cutting edge
When timing the cutting edge, firstly ensure the consistency of the cutting edge of the trimming knife block to avoid parts cutting. Because the cutting is easy to produce aluminum strips at the same time, it can ensure that the parts are cut at the same time to reduce the cutting chips. The cutting depth is controlled to about 3mm, and the friction between the knife edge and the parts is reduced to reduce the generation of chips.
Edge shape
The cutting edge and trimming edge should not be too sharp. Use a file or whetstone to polish the cutting edge block and trimming edge so that the edge has a rounded corner of about 0.2mm to avoid the edge being too sharp. If not, the aluminum plate tends to be broken during the trimming process. Will produce a larger fracture zone.
Heat treatment of molds and inserts
According to reference foreign standard parts manual. The surface of the knife block is coated with a beryllium layer, which can improve the wear resistance of the knife block. Increasing the finish of the insert increases the hardness of the insert, which can avoid the generation of waste. Reduce mold maintenance.
For the OP10 drawing die, because it is a forming process, the material flows in the molding surface. It is inevitable that long-term work will cause the material to fall off and stick to the ratting tendons, which will also produce debris. For this problem, we applied electroplating to the mold. Increase the finish of the mold. It prevents debris from being rubbed, and also increases the hardness of the mold to prevent damage to the mold caused by napping.
For OP20/30/40 molds, we compare traditional electroplating and TD processing, and finally adopt PVD technology. Compared with electroplating, PvD has a higher degree of wear resistance. Compared with TD processing, the processing temperature of PVD is lower, about 240-350℃, which has a good control effect on the deformation of the insert.
Hot Tags: Cnc Aluminum Keyboard Parts Electronic Keyboard Enclosure, China, manufacturers, suppliers, factory, wholesale, customized, made in China
Send Inquiry
You Might Also Like


